OEM Carbonated Beverage Production Line Maker Key Factors to Evaluate Before You Invest
2026-09-28
Every bottle of sparkling soda on the shelf is the result of a complex production chain—and the weakest link in that chain can drain your investment faster than a leaky carbonation tank. Before you sign with an OEM carbonated beverage production line maker, you need to look beyond glossy brochures and price tags. This guide breaks down the factors that truly determine line reliability, output quality, and long-term ROI. At INTOP Machinery, we've seen how the right evaluation saves buyers from costly downtime—and we're sharing those insights here.
Pressure, Fill Speed, and Carbonation Consistency Under Real Loads
When the line runs at full tilt, the interplay between pressure, fill speed, and carbonation stability becomes impossible to ignore. Most machines hold their specs on a test bench, but real production throws variables—temperature swings, pump pulsation, back-pressure from downstream equipment—that quickly expose weak points. The goal is not just hitting a pressure number, but keeping the CO₂ in solution while the filler valve cycles faster than the gas can escape.
A common failure mode is cavitation at the fill head when tank pressure dips during high-demand bursts. That momentary drop lets dissolved gas break out, leading to inconsistent fill levels and foam-over. Properly sized supply lines, surge capacity, and a control loop that anticipates rather than reacts are what separate a line that runs clean at 600 bottles per minute from one that needs constant babysitting.
Measuring carbonation consistency under load means sampling at the filler, not just at the tank. Slight variations in fill speed change residence time in the bowl, which shifts CO₂ pickup. Operators who chase the pressure gauge alone often miss the real issue: the relationship between throughput and gas solubility is nonlinear, and holding it flat across a shift requires both mechanical headroom and smart tuning.
How Will the Maker Handle Your Recipe's Foaming Quirks?
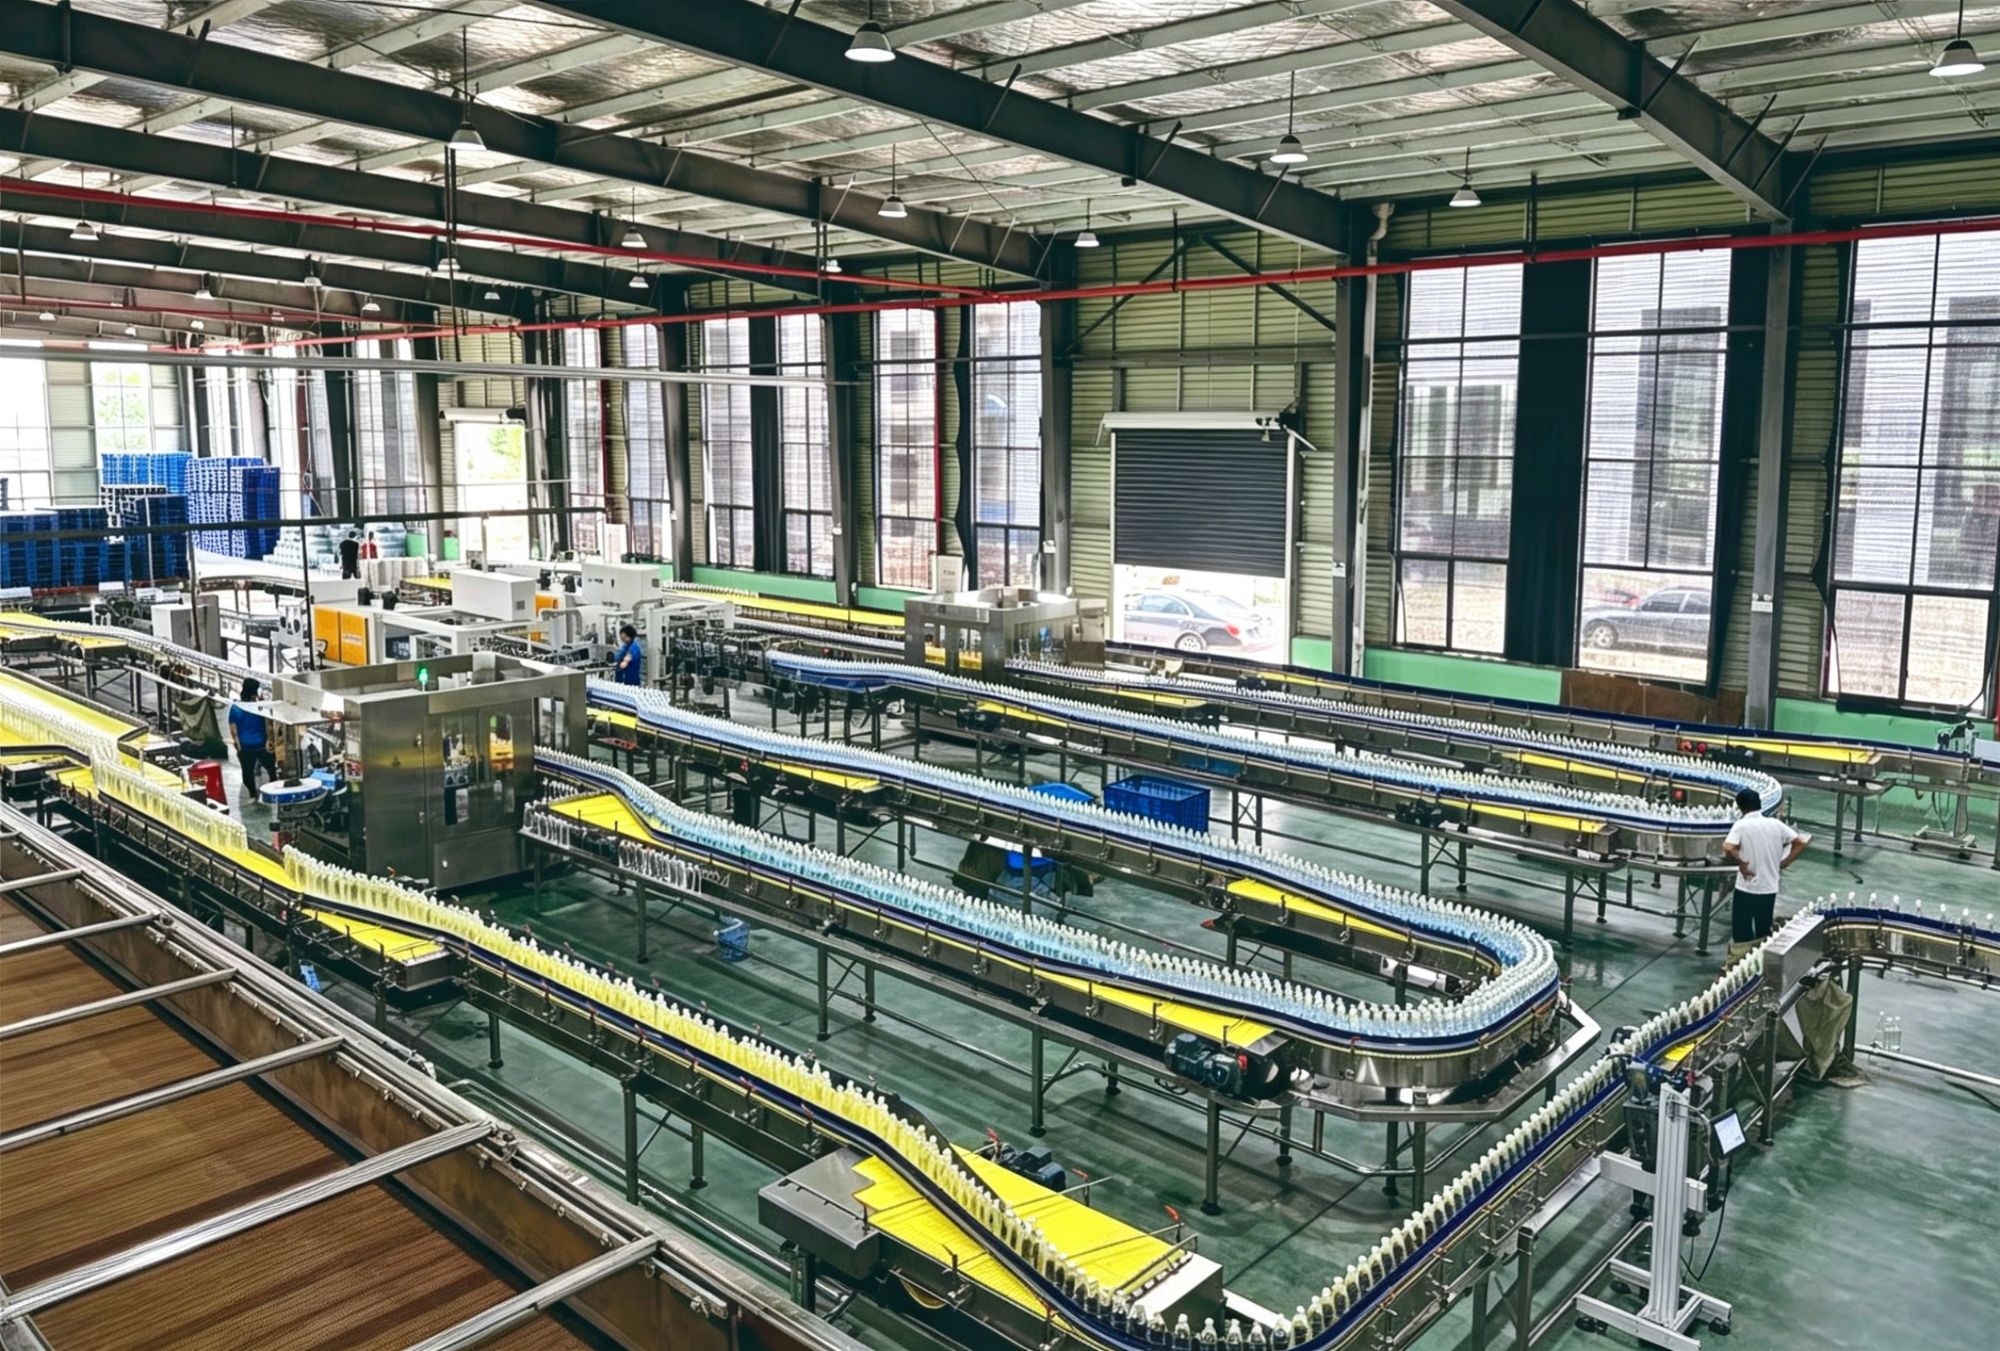
The maker doesn’t just churn through your recipe blind. It watches for that telltale creaming or bubbling at the surface, then eases the paddle speed or pauses briefly so air pockets can settle. You won’t need to babysit it with a towel or stir in defoaming drops.
If a recipe tends to foam early—like ones heavy on fresh fruit or dairy—the machine pulls back on heat just enough to keep the rise from boiling over, then resumes the programmed cycle once the foam has collapsed. That quiet adjustment is what saves you from a sticky mess and gives you a smoother final texture.
The Real Cost of Downtime: Spare Parts Availability and Lead Times
When a production line halts, the financial bleed is rarely visible in a single ledger entry. It shows up in overtime wages, expedited shipping fees, and the quiet erosion of customer trust. Yet many managers only tally the price of the failed component itself, ignoring how a missing $50 bearing can idle a $500-per-minute operation for days.
Spare parts availability turns out to be less about warehouse size and more about decision quality. A plant that stocks hundreds of low-failure items while waiting weeks for a critical motor drive is not prepared—it is merely busy. The real metric is not inventory value but recovery time: how quickly can you source, ship, and install the one part that actually stops the line.
Lead times compound the problem in ways that static reports miss. A quoted three-week lead for a gearbox may stretch to six if the supplier itself waits on a casting from a sub-tier vendor. Each day of delay adds not just direct production loss but also the cost of idle labor, missed delivery penalties, and the subtle shift of orders to competitors who happened to have the part on the shelf.
Do Their Certifications Cover Every Market You Plan to Enter?
Many suppliers will list certifications like CE, RoHS, or FCC, but these do not automatically grant access to every country. A certificate issued for the European Union often carries little weight in markets such as Brazil, South Korea, or Saudi Arabia, where local approvals are mandatory. If you plan to enter multiple regions, ask for a breakdown of which specific certificates apply to each target country.
Even within a single certification framework, variations exist. For example, a product certified under IEC standards may still require national deviations to be accepted in Japan or China. Relying on a general statement like "internationally certified" can lead to unexpected customs delays or rejected shipments. Request the actual certificate numbers and verify their scope directly with the issuing bodies or your local compliance partner.
The most practical approach is to provide the supplier with your exact entry list before finalizing the order. Let them confirm in writing which certifications they currently hold for each market, and which ones would require additional testing or fees. This eliminates guesswork and keeps your launch timeline realistic.
From Line Layout to Staff Training: Where Custom Projects Usually Slip
Most custom work starts with a detailed drawing of the line layout. Teams spend days adjusting conveyor angles, workstation spacing, and material flow. Then the build begins and everything looks right on paper. The first slip often happens here: nobody walks the actual floor with the operators before the equipment arrives. A pillar that wasn't in the model, a drain cover that makes cart movement rough, or a cable tray that blocks sightlines can force last-minute changes. These small physical clashes are rarely dramatic, but they eat into the schedule in a way no Gantt chart captures.
The second common failure point moves from the line to the people. After the physical installation is done, training is treated as a one-time event. Staff get a quick overview, maybe a binder, and then they're expected to run at full speed. But custom projects rarely run at full speed on day one. The real learning happens when a sensor trips, a part jams, or a changeover is due. If the training doesn't include those messy, non-standard moments, the team will learn by breaking things. That's where a supposedly finished project starts to slip backward.
Another overlooked gap is the handoff between layout changes and training materials. When the line is adjusted during commissioning, the work instructions are often updated later, or not at all. An operator who follows an outdated guide will make the line look like it failed, when the process simply drifted. Keeping one person responsible for walking the line after each change and updating the training docs the same day closes that loop. It's not glamorous, but it prevents the slow decay that turns a promising custom build into a permanent bottleneck.
Comparing Total Cost of Ownership, Not Just the Quote
Many buyers fixate on the initial quote because it looks easy to compare side by side. But that number rarely reflects what you'll actually pay over the life of the asset. Energy consumption, maintenance intervals, spare parts pricing, and unplanned downtime can each swing the final figure by double digits. A machine quoted $10,000 lower might need twice the servicing and consume 30% more power, erasing the upfront savings within the first year.
To compare total cost of ownership accurately, pull operational data from your existing fleet instead of relying solely on vendor spec sheets. Ask for maintenance logs, actual energy usage from similar installations, and common failure rates. Then model those costs over the ownership period you have in mind. This shifts the buying conversation from "Who has the cheapest sticker price?" to "Which option leaves more cash in the operating budget at year five?" That is the number that deserves attention.
FAQ
Look beyond marketing claims. Ask for a list of recent installations that match your production volume and container type. Contact two or three of those buyers directly and ask about downtime frequency, how quickly spare parts arrived, and whether the line hit promised speeds during commissioning. A maker with real experience will share references without hesitation.
It depends on their engineering depth. A good partner will map your specific bottle shape, carbonation level, and filling temperature into the line design instead of forcing a standard layout. Ask whether they modify filler valves, rinser nozzles, and conveyor widths in-house or just assemble bought-in modules. The former usually delivers smoother startups.
Carbonated beverage lines run long shifts, so a small difference in per-bottle energy use adds up fast. Request utility consumption data for air, water, and electricity at your target output. Compare figures from at least two makers, but make sure the data covers the same scope—some exclude compressors or chillers to look better.
For most markets, look for ISO 9001 as a baseline and food-contact material compliance such as FDA or EU 1935/2004 depending on where you sell. If you export to specific regions, ask for CE marking, UL listing, or local safety approvals. Don't accept vague statements—ask for certificate numbers and verify them.
Build a three-year cost model that includes spare parts, preventive maintenance, expected wear items like seals and filling valves, and energy use. Ask the maker for a recommended spare parts list with prices and lead times. A line that costs less upfront can become expensive if key parts are proprietary and slow to ship.
Support determines how quickly you recover from a breakdown. Ask about response time guarantees, remote diagnostics, and whether technicians can reach your plant within a set window. Check where their nearest service hub is and how many engineers cover your region. A distant support team can turn a one-day stoppage into a week-long loss.
Yes, and not just the showroom. Walk through the assembly area, look at the quality of welding and component storage, and ask to see a line being tested with actual product before shipping. If a visit is impossible, request a live video walkthrough of a current build and a full factory acceptance test plan.
Very important. Ask which brands they use for PLCs, drives, fillers, and carbonators. A line built around widely available components from Siemens, Allen-Bradley, or Mitsubishi is easier to service locally. Avoid makers that use obscure or rebranded parts without a clear source, because you may face long waits when something fails.
Conclusion
A production line that performs flawlessly in a demo can fall apart under real operating conditions, so push the OEM for evidence of pressure stability, fill speed, and carbonation consistency when the system is running at full capacity with your actual product—not water. Ask specifically how they plan to manage your recipe's foaming quirks, because a beverage that froths excessively during filling will create inconsistent volumes, waste, and endless line stoppages. Equally important is the maker's spare parts strategy: if a critical valve or sensor fails, a two-week lead time can shut down your entire operation. Look for regional part stock, clear replacement timelines, and a service response that matches your production schedule.
Beyond the machine itself, verify that the OEM's certifications align with every market you intend to enter—food safety and electrical standards vary widely, and retrofitting a line later is expensive. Custom projects often slip during the transition from line layout to staff training, so get written commitments for installation milestones, operator handover, and ongoing support rather than relying on a single sales presentation. Finally, compare total cost of ownership instead of fixating on the quoted price: energy consumption, maintenance intervals, changeover downtime, and expected component lifespan will determine whether a cheaper line ends up costing far more over five years. A detailed, transparent TCO breakdown from the maker is a strong sign you are dealing with a partner, not just a supplier.
Contact Us
Contact Person: Laura
Email: [email protected]
Tel/WhatsApp: +86 13957758832
Website: https://www.intopmachinery.com