Stainless Steel D Shackle Factory: Inside Precision Manufacturing and Quality Control
2026-10-18
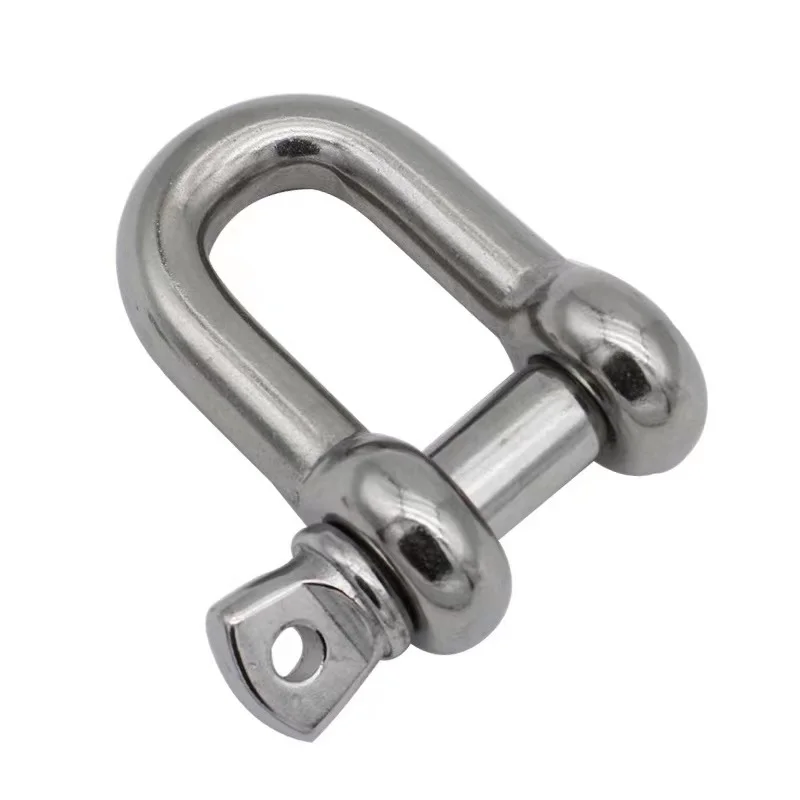
Walk into most hardware aisles and a D shackle looks like a commodity. At Wanluo’s stainless steel D shackle factory, nothing could be further from that. Every batch starts with spectro-verified 316 steel, passes through CNC-machined pin bores, and ends with proof-load testing beyond the rated WLL. This inside look shows why the quiet details—thread tolerances, surface finish, heat lot records—separate hardware that holds from hardware you hope holds.
Raw Stainless, First Inspection at the Gate
Rolled coils arrive shrouded in mill wrap, and the gate check starts before the truck even cuts its engine. A quick walk-around flags anything that shifted in transit—dented edges, torn packaging, moisture trapped under the film. The receiving clerk verifies the heat number against the mill certificate right there, matching the stencil on the coil's side. If that number doesn't line up, the load stays outside.
Once the paperwork clears, the metal gets a closer look under natural light. Surface defects like scale pits, scratches, or edge waves don't hide well on raw stainless. Thickness and width are spot-checked with calipers and a tape, not just trusted from the data sheet. Any coil with more than superficial staining is set aside for a full inspection before it ever reaches the rack.
Forging the Bow Without Weak Points
A bow is only as reliable as its most neglected inch. When I rough out a stave, I mark every ring violation or pin knot before the drawknife touches wood, then chase a single growth ring across the back so the fibers run unbroken from tip to tip. That continuity is what stops a bow from hinging or blowing up under full draw. If the stave has a wavy grain, I follow those waves instead of forcing a straight line, because a sharp angle across the grain creates a ready-made weak point.
Tillering is where most weak points show themselves, and it usually comes down to impatience. I scrape a few passes from a stiff spot, exercise the limbs thirty times, then put the bow back on the tree. The goal is a smooth, even arc at every inch of draw, but the real test is watching the tips after unstringing: if one tip has crept forward, that limb has taken a set and I need to ease tension there or lightly heat-treat the belly. A bow that bends only in the middle may feel quick at first, but it will chrysal or break because the outer limbs are doing nothing.
Backing and overlay work fill the final gaps. A thin rawhide or sinew backing over a violated ring can hold splinters down, but it will not fix bad tiller. At the nocks, I keep the string grooves smooth and round, because a sharp notch under tension is a fracture waiting to happen. Once the bow has a few hundred arrows through it, I re-check the brace height and twist the string back to spec. That kind of quiet maintenance is what keeps a bow without weak points shooting straight past the first season.
Machining the Pin to a Few Microns
Holding a pin to within a few microns isn't something you achieve by simply dialing in a lathe and hoping for the best. It starts with understanding that thermal drift alone can eat up your tolerance before the tool even touches the metal. We always let the spindle and the workpiece reach a steady temperature before the finishing passes. That means running the machine at idle for ten or fifteen minutes, then taking a light skim cut and measuring with a micrometer that has its own temperature compensation. Without that step, the numbers you see on the readout are fiction.
The actual cutting strategy matters just as much as the prep. Instead of hogging the diameter down in one aggressive pass, we leave about twenty microns of stock and switch to a fresh, sharp insert with a very small nose radius. The feed rate drops to almost nothing, and the depth of cut is so light that it feels like polishing. This avoids pushing the material around and creating a false surface that springs back after you unclamp the part. Finally, we measure the pin in the same orientation it will be used, because even a few microns of ovality can show up as a tight spot during assembly.
There's also the human element that rarely appears in textbooks. If you chase the final dimension too aggressively, you end up chasing your own tail—taking off a micron, remeasuring, taking off half a micron, and suddenly overshooting because of a tiny burr. A far better approach is to stop about two microns over, then use a fine diamond lap or a strip of abrasive paper to bring the pin down by feel. It sounds old-fashioned, but with a steady hand and a good optical comparator, you can hold a diameter more consistently than any automated compensation algorithm.
Why Every Shackle Gets Its Own Serial
A shackle is more than a bent steel loop—it's a critical load path in lifting and rigging. Every unit carries its own serial because traceability matters when something goes wrong. If a shackle fails under load, that number links it to the exact heat of steel, the forging batch, and the proof test record. Without it, you'd be left guessing whether an entire production run shares a hidden defect. The serial keeps the failure isolated, not systemic.
On a job site, marks get scraped off and paint wears away, but the serial remains stamped where it counts. Inspectors rely on it during daily checks and after any overload event. Instead of sidelining a dozen identical shackles because one looks questionable, the serial lets you pull the specific unit's history—when it was made, when it was last tested, and what it has been through. That level of accountability is what separates a controlled lift from a dangerous guess.
Proof Testing Before It Leaves the Floor
A pressure gauge on a hydraulic power unit can read perfectly at rest, yet fail the moment the system builds to working pressure. That is why proof testing before a machine leaves the shop floor goes far beyond a visual once-over. Every hose, fitting, and valve gets cycled through its full operating range—sometimes beyond it—to catch the kind of hidden weakness that only shows up under real load. A slow seep at a banjo bolt, a solenoid that sticks when warm, a relief valve that chatters instead of opening cleanly: these are the defects that turn a finished assembly into a warranty claim if they ship unnoticed.
The test bench itself is often built as ruggedly as the equipment being tested. Technicians follow a written sequence that includes deadheading pumps to confirm relief settings, holding cylinders at full extension for a set dwell time, and cycling directional valves hundreds of times while logging pressure drop and temperature rise. One common step is a cold-start simulation: the unit sits overnight in an unheated bay, then gets fired up and run through its motions before the oil warms. Another is a contamination check that draws a fluid sample after the test and counts particles under a microscope—anything over ISO 18/16/13 fails the unit on the spot. These procedures are not glamorous, but they are the difference between a machine that works on paper and one that works in the field.
The final sign-off often includes a witnessed test for critical customers, where an inspector watches the machine lift a proof load or hold a test pressure for a specified number of minutes. Test results get recorded on a serial-number-specific data sheet, not just a generic checklist. If a pump later fails in service, the factory can pull the original performance curve and see whether it drifted from day one. This kind of traceability builds trust without a single marketing claim. When a buyer sees a scuffed test port and a stack of dated run logs, they know the machine did not just roll off the line—it earned its way off the floor.
Surface Finish That Fights Corrosion
A surface finish isn't just about looks. The right texture and coating system can actively block moisture, oxygen, and chloride ions from reaching the base metal. Think of it as a physical shield: a tightly sealed, low-porosity layer leaves fewer entry points for corrosive agents to settle and start their work. In marine or industrial environments, this kind of barrier becomes the first line of defense, often outperforming thicker, rougher finishes that trap contaminants.
Some finishes go beyond passive protection. Sacrificial coatings, such as zinc-rich primers or aluminum sprays, corrode preferentially to the underlying steel. Others use passivation—converting the surface into a stable oxide layer that resists further attack. The key is matching the finish to the exposure: a polished, non-porous chrome plating works wonders on hydraulic rods, while a textured epoxy coating grips better on structural beams without sacrificing corrosion resistance.
Maintenance also changes the game. A smooth finish with minimal crevices is easier to clean and inspect, so early signs of pitting or discoloration don't hide in rough valleys. By combining the right profile, coating chemistry, and upkeep routine, you create a surface that doesn't just endure—it actively fights back against corrosion year after year.
FAQ
Most reputable factories use AISI 316 stainless steel for marine-grade shackles because of its superior corrosion resistance, especially in saltwater environments. Some also offer 304 stainless steel as a more economical option, but 316 is the default for critical lifting and rigging applications. The raw material is usually sourced as forged blanks or bar stock, and each batch is verified with a spectrometer before machining begins.
Precision starts with CNC machining centers that hold tolerances within ±0.05 mm on the pin bore and shackle throat. After machining, every shackle passes through a coordinate measuring machine (CMM) or a dedicated go/no-go gauge set. The critical dimensions—like the jaw opening, pin diameter, and crown thickness—are checked against the working load limit specification, not just the nominal size.
Heat treatment is what separates a load-bearing shackle from a decorative one. For stainless steel, solution annealing is performed at around 1040°C followed by rapid water quenching to dissolve carbides and restore corrosion resistance. Some factories also apply a sub-zero treatment for dimensional stability. Without proper annealing, the shackle can suffer from stress corrosion cracking under load.
Each production lot undergoes a proof load test, typically at 2 times the working load limit, where the shackle is held under tension for a set period and then inspected for permanent deformation. Additionally, magnetic particle inspection or dye penetrant testing is done on the pin and crown areas to detect surface cracks. For high-volume orders, a sample from every heat number is also sent for destructive tensile testing to confirm the breaking strength meets or exceeds the minimum requirement.
The most common finish is electro-polished, which removes a thin layer of surface metal and creates a smooth, passive layer that resists pitting and crevice corrosion. Some factories offer a mirror polish for architectural or yachting applications, while others apply a passivation treatment only. The choice depends on the environment—electro-polishing is strongly recommended for offshore and chemical exposure because it reduces the surface roughness where chlorides can accumulate.
Traceability is maintained through heat numbers and batch codes. Each shackle is laser-marked with a unique serial number that links back to the mill certificate of the stainless steel bar or forging. The factory keeps digital records of the chemical composition, heat treatment furnace logs, and test reports for at least 10 years. This allows auditors or end users to verify that the material meets ASTM or EN standards, even years after purchase.
The key differences are in the details: a precision shackle has a machined pin with a rolled thread rather than a cut thread, which eliminates stress risers; the pin bore is honed to achieve a close sliding fit without play; and the working load limit is permanently marked on the body, not just on a tag. Generic shackles often skip the proof load test entirely and use lower-grade stainless steel that can gall or seize under load.
For lifting and rigging, a factory should at minimum have ISO 9001 for quality management, and ideally product certification from a notified body like DNV, ABS, or Lloyd's Register for marine use. In Europe, CE marking under the Machinery Directive is mandatory for shackles sold as lifting accessories. A reputable factory will also have in-house testing equipment calibrated to ISO 17025, and they should be able to provide a Declaration of Conformity with every shipment.
Conclusion
Walking into the D shackle facility, the first thing you notice is that nothing gets through the gate without a hard look. Raw stainless bars are checked for grade, surface flaws, and dimensional drift before they ever touch a forge. From there the bow takes shape under controlled heat and pressure, with the grain flow worked so there are no hidden weak points at the crown or the ears. The pin is not just turned; it is machined to a tolerance of a few microns, then matched to its own bow. That pairing is why every shackle gets an individual serial number, not as a marketing gimmick but so the exact heat lot, machine settings, and operator can be traced back years later.
Before anything leaves the floor, each unit is proof tested to a load well beyond its working limit, and only the ones that hold without permanent deformation move on. The final surface treatment matters just as much as the forging itself. A passivated, polished finish is applied to fight pitting and crevice corrosion in saltwater and chemical environments. That combination of raw material inspection, precise machining, traceability, proof loading, and corrosion-resistant finishing is what separates a load-rated D shackle from a cheap lookalike. It is slow, repetitive work, but when a lifting failure is not an option, the factory would rather over-check than ship a weak link.
Contact Us
Contact Person: Shane
Email: [email protected]
Tel/WhatsApp: 8613357785029
Website: https://www.wanluohardware.com