Top Tumble Shot Blasting Machine Manufacturer - A Comprehensive Buyer's Guide
2026-10-13
Finding a reliable tumble shot blasting machine manufacturer can feel like navigating a maze of inflated claims and disappointing performance. If you’ve been burned by machines that break down mid-cycle or leave inconsistent finishes, you’re not alone. This guide cuts through the noise—no fluff, no recycled sales copy. We’ll walk you through what actually matters: build quality, blast efficiency, maintenance reality, and the questions most buyers forget to ask. Among the names worth your attention, PuHua stands out for its reputation in durable, high-precision systems. Whether you’re upgrading a single workstation or outfitting an entire line, the right choice starts here.
What Tumble Blasting Does That Other Methods Can't
Tumble blasting reaches corners, recesses, and intricate profiles that wheel blasting or hand tools simply miss. Because parts move continuously inside the chamber, the media wraps around every edge and blind hole, producing a uniform finish without operator-dependent variation.
Another noticeable difference is the absence of thermal or mechanical stress. Processes like grinding or aggressive sanding can warp thin sections or leave heat marks, but tumbling relies on low-energy impact across the whole surface. Delicate stampings, springs, and sintered parts come out clean without bending or losing dimensional accuracy.
It also handles large batches with a consistency no manual finishing can match. A single cycle processes hundreds of small components at once, and every piece receives the same exposure to the media. That makes it suitable for deburring, descaling, and preparing surfaces for coating when other techniques would either damage the parts or take far too long.
The Design Details That Separate Real Workhorses from Pretenders
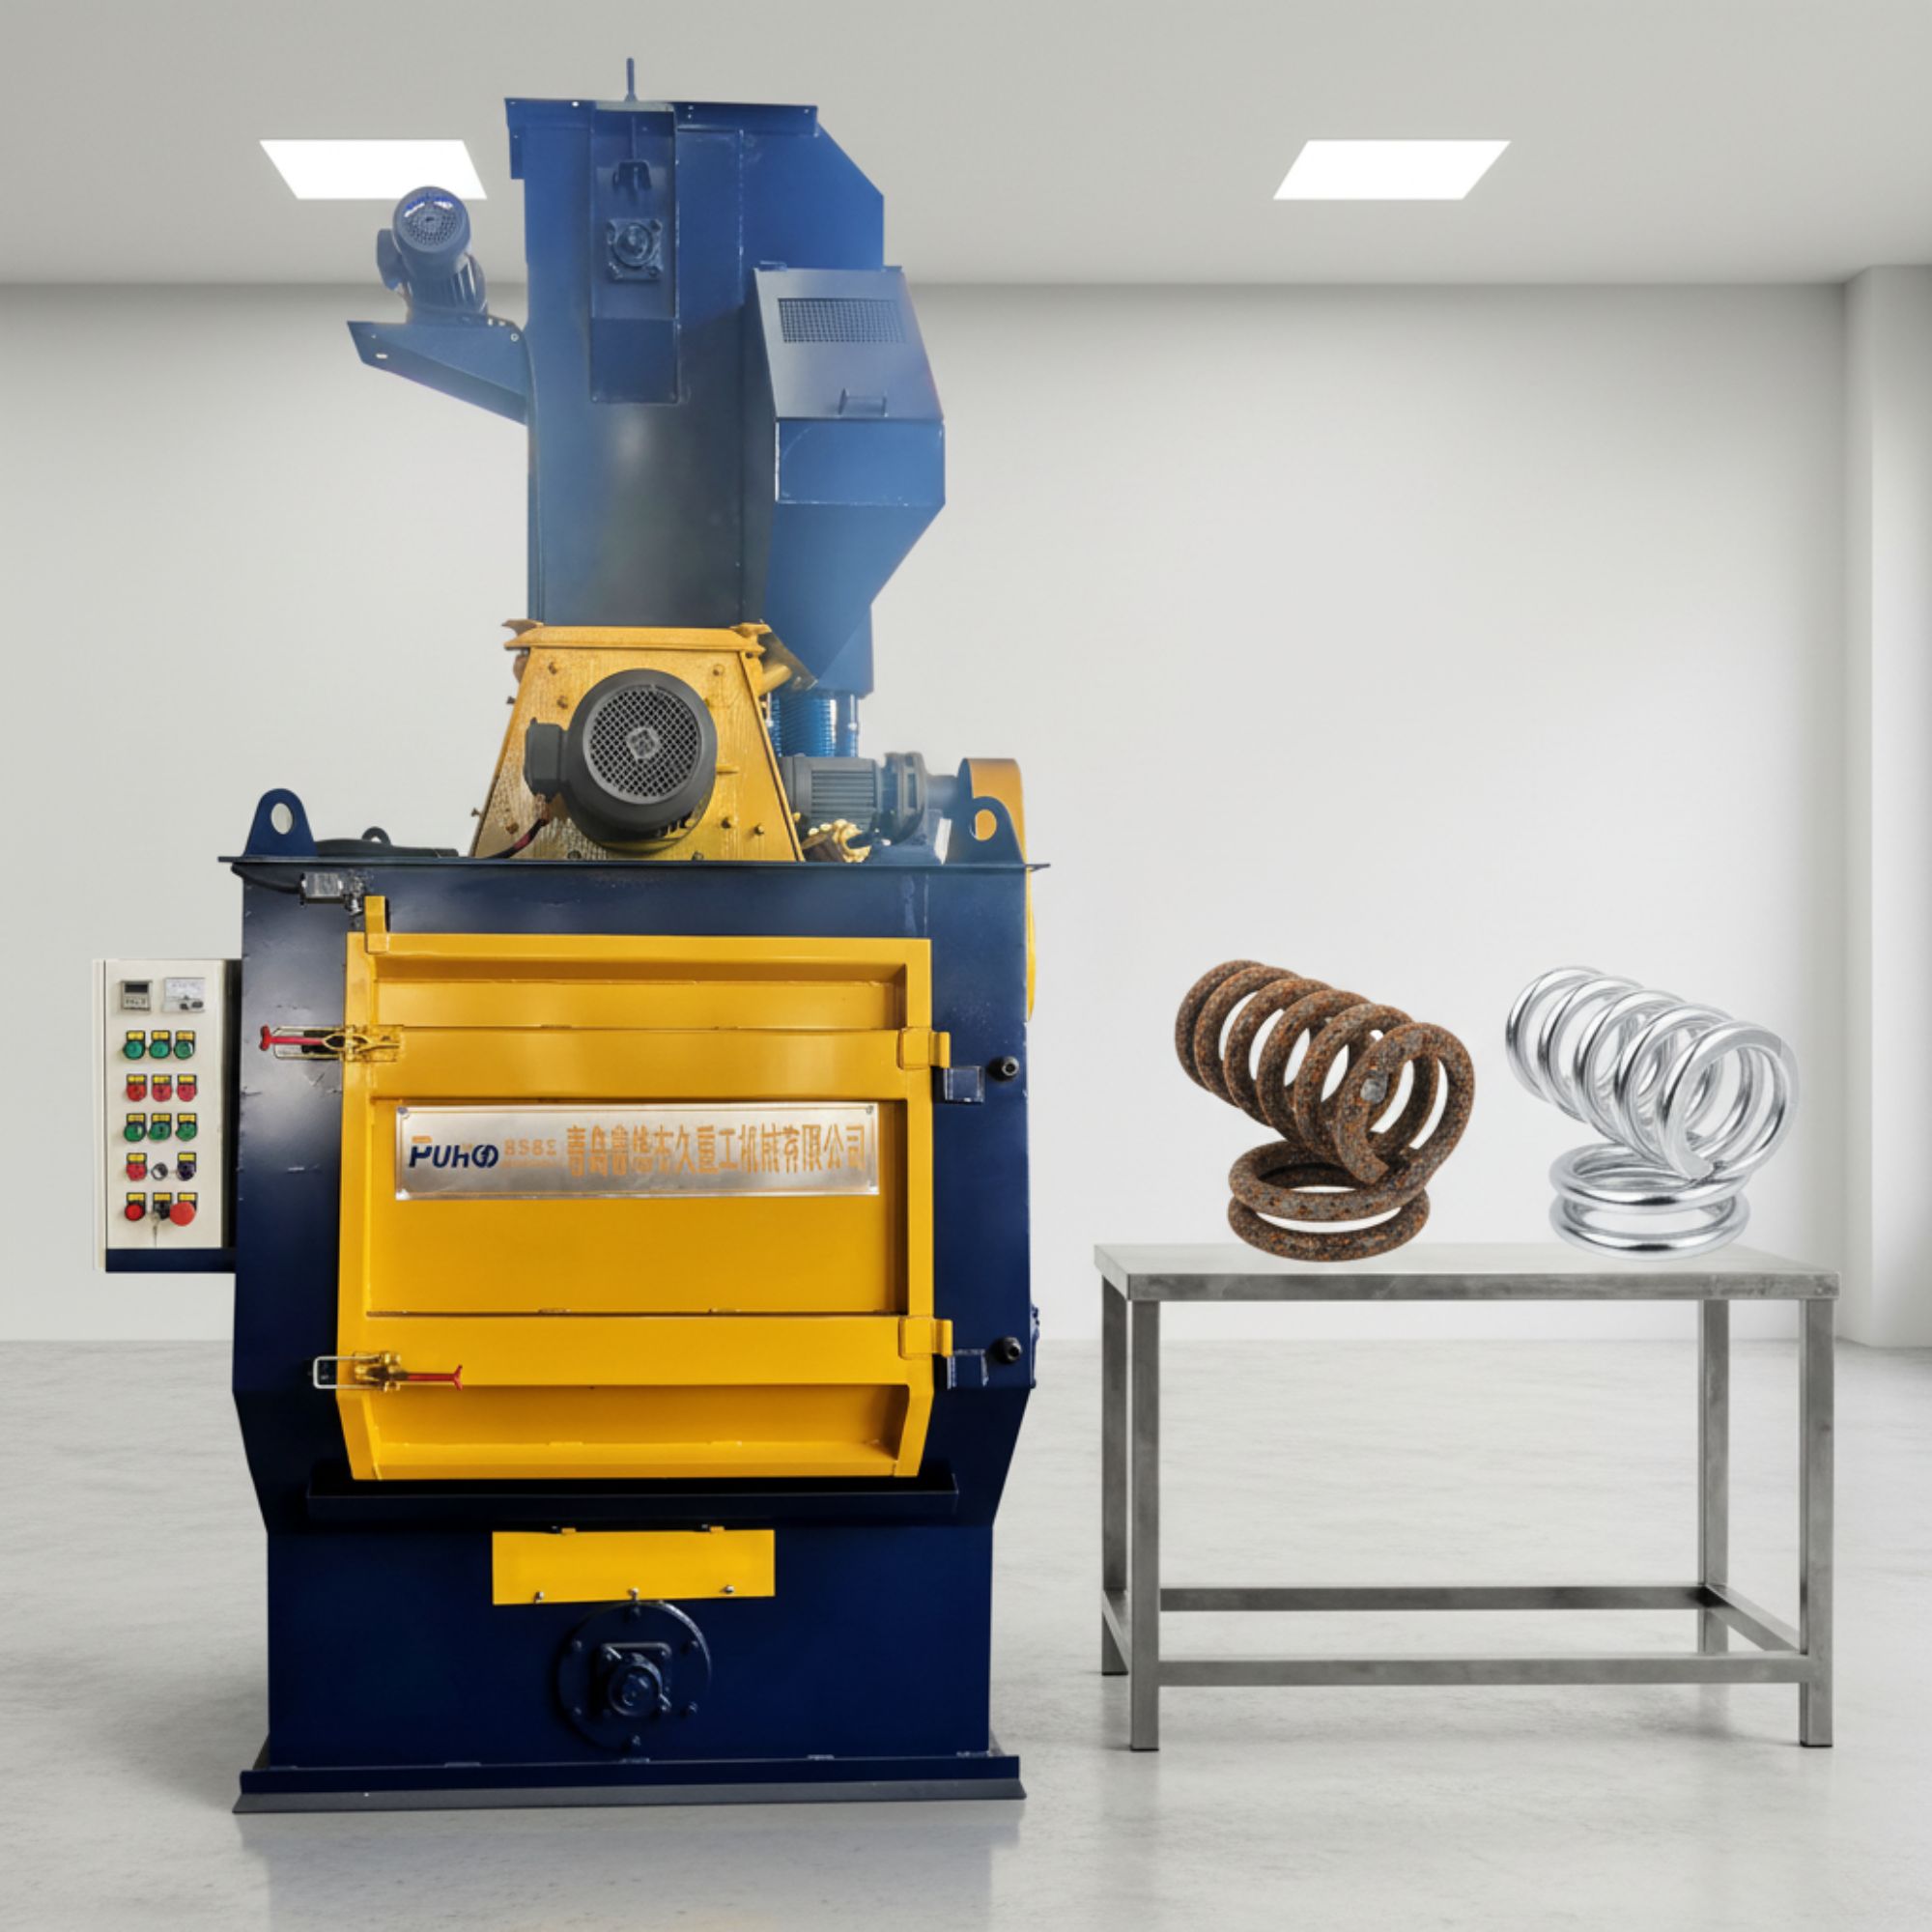
Look closely at the pivot points and load paths. Real workhorses don't hide their bones—they show evidence of extra material where stress concentrates. You'll see double-stitched seams that follow the contour of a handle instead of cutting across it, or a hinge that's machined from a single billet rather than stamped and spot-welded. Pretenders tend to coat everything in a uniform layer of 'rugged' texture, but the giveaways are the small transitions: a cable exit that lacks a strain relief, a clasp that flexes under thumb pressure, or a foot pad that's glued on instead of mechanically locked.
Another tell is serviceability. A true workhorse is designed to be taken apart with common tools, because the people who depend on it expect to replace a worn bushing or tighten a fastener after five years of hard use. If you find hidden snap tabs that break when you open the housing, or screws buried under rubber caps that disintegrate, you're looking at a product meant to be replaced, not repaired. That gap between 'looks tough' and 'stays tough' almost always shows up in the details nobody photographs.
Choosing a Machine That Fits Your Parts—Not the Other Way Around
A machine's table size, travel, and spindle nose clearance aren't abstract specs—they're physical boundaries your parts live inside. If you have to shim a fixture, swap jaws twice, or rotate a part mid-cycle just to reach a feature, that machine is already costing you in setup time and scrapped prototypes. Start instead with a list of three to five parts you actually run, note their dimensional extremes, and use that as your filter.
The same logic applies to material and tolerance. A machine built for hogging cast iron won't automatically shine on thin-wall aluminum, and a high-speed drill-tap center may struggle with hard-to-machine alloys. Match spindle power, rigidity, and thermal stability to the work you do most often, not to a hypothetical future job. If most of your parts are within a narrow size range, buying extra travel just in case means paying for floorspace and accuracy you don't need.
Finally, think about the entire workflow, not just the cutting. Can the operator load parts without leaning over a deep table? Does chip evacuation work for your material? Will your existing toolholders and CAM posts transfer over without a fight? When a machine fits your parts, these daily details feel boringly easy. When it doesn't, every job turns into a workaround. Choose the machine that disappears into the background of your process.
How to Spot a Manufacturer That Actually Knows Surface Finishing
Ask them what happens when a finish fails. A manufacturer that actually understands surface finishing won't just blame the plating bath or the powder coating oven—they'll walk you through their incoming inspection, pre-treatment steps, and the specific instruments they use to check roughness, coating thickness, or corrosion resistance. If they can't name the exact measurement tools or the tolerances they hold on adhesion and gloss, that's a red flag.
Pay attention to how they talk about difficult parts. The real experts get animated about masking threaded holes, racking weird geometries, or handling mixed-material assemblies. They'll mention things like Faraday cage effects in anodizing, outgassing in powder coat, or the risk of hydrogen embrittlement on high-strength fasteners—not because they're showing off, but because those details matter. A shop that says "we can do any finish" without asking about substrate, size, or end-use environment is guessing.
Finally, ask for a process control plan, not just a glossy brochure. A competent finisher will share how they track bath chemistry, oven temperature uniformity, or blast media breakdown over time. They'll likely have records of salt spray tests or cross-hatch adhesion results for your specific alloy or plastic. If they hesitate or hand you a generic certificate, keep looking.
The Price Tag Is Just the Beginning: Long-Term Costs Explained
A tempting sticker price can feel like the end of the decision, but for most purchases it’s only the opening scene. The real cost shows up later in the form of electricity, fuel, insurance, replacement parts, and routine upkeep. A budget-friendly laptop might need a battery swap after eighteen months, while a modestly priced car could demand premium fuel and pricey tire replacements. When you only compare the numbers on the tag, you miss the quiet drip of ongoing expenses that often outweigh the initial savings.
Resale value and depreciation also shift the math more than people expect. Two products can cost nearly the same today, yet one may hold its value far better over three or five years. If you plan to sell or trade in, that gap becomes real money in your pocket — or out of it. Add in financing charges and the timing of major repairs, and the cheapest option at the register can turn into the most expensive one to live with over time.
Maintenance Routines That Keep Your Blast Machine Running for Decades
Most blast machine failures trace back to neglected daily habits rather than major component defects. Spending ten minutes at the end of each shift to blow down the cabinet, check the view window for pitting, and inspect the nozzle for irregular wear can catch small problems before they turn into expensive rebuilds. Keep a simple log near the machine—note air pressure, media condition, and any unusual vibration. That record becomes your best diagnostic tool when performance starts to drift.
Media quality matters more than many operators realize. Reclaimed abrasive breaks down over time, turning sharp cutting edges into dust that clogs filters and slows cleaning. Sift or replace media on a schedule tied to actual blast hours, not guesswork, and make sure the separator is adjusted so it removes spent fines without dumping good grit. Pair that with monthly checks on hoses, gloves, and door seals. A tiny air leak in a worn glove or a cracked hose not only wastes compressed air but also invites contamination into the cabinet.
Long-term survival comes down to respecting the machine's lubrication and filtration points. Drain moisture from the air supply daily, replace filter elements before they cake over, and grease bearings and pivot points with the manufacturer's recommended intervals. When you do replace wear parts, use matched sets—nozzle, air jet, and window film—so the system stays balanced. Machines that receive these small, consistent attentions often outlast the original purchase paperwork by a wide margin.
FAQ
These machines really shine with castings, forgings, stampings, and machined components that need descaling, rust removal, or a uniform matte finish before coating. The rotating drum keeps parts gently tumbling while abrasive is thrown at them, so it works well for parts that can withstand some movement and impact—think brackets, gears, housings, and small to medium hardware. For very fragile or thin-walled components, you'd want to test the process first or ask the manufacturer about low-impact media options.
Start by looking at your largest batch size and average daily output, not just the machine's total volume rating. A good rule of thumb is to keep the load between 40% and 60% of the drum's working volume so parts have enough room to tumble without bruising each other. Also factor in the abrasive weight—it can double the effective load. If you're running mixed part sizes, talk to the manufacturer about a test run to confirm cycle times and batch weights.
Beyond the spec sheet, pay attention to how they handle engineering details: the blast wheel design, thickness and material of the wear plates, how well the media recovery system works, and whether the dust collector is sized correctly. Ask for customer references in your industry or a factory visit if possible. A manufacturer that pushes back on your part drawings and suggests process adjustments is often more valuable than one that just quotes the lowest price.
You'll be replacing liners, blast wheel blades, impellers, and screens on a regular schedule depending on how many hours per day the machine runs. As a rough starting point, set aside 5–10% of the equipment purchase price per year for consumables and unexpected wear items. Ask the manufacturer for the expected life of each wear part in operating hours, and check whether they keep local spare parts stock or can ship quickly.
Yes, and it's often easier than people expect. Most reputable manufacturers offer options like automatic loading hoppers, vibratory feeders, discharge conveyors, and even robot pick-and-place interfaces with PLC controls. The key is to discuss your upstream and downstream processes early—parts orientation, cycle time matching, and control signal compatibility all need to be defined before the machine is built. A well-integrated tumble blaster can run unattended for hours if the media level and dust collector are monitored automatically.
Abrasive blasting generates a lot of fine dust, so you'll need either a dry cartridge-type dust collector or a wet scrubber, depending on your material and local emission rules. Don't undersize the collector—aim for enough airflow to keep a slight negative pressure inside the blast chamber so dust doesn't leak into your shop. Ask the manufacturer to supply the complete system as a package, because a mismatched dust collector is one of the most common reasons these machines underperform.
Absolutely, and I'd treat it as a must-do for any new part family. Sending samples to the manufacturer's lab or arranging a demonstration with your own parts lets you verify cleaning quality, identify any risk of edge rounding or damage, and get a realistic cycle time. Many companies will even fine-tune the abrasive type and blast intensity during the test, which gives you a much clearer picture of what the machine will do in your facility.
Conclusion
When shopping for a tumble shot blasting machine, the real question isn't whether it cleans parts—it's whether it can handle the awkward, mixed batches that cabinet or pass-through systems leave behind. Tumble blasting throws parts and media together in a rotating drum, letting the abrasive reach hidden pockets, threads, and flat faces without operator repositioning. That capability alone changes how a job shop quotes work. But not every drum is built to last. The difference between a workhorse and a pretender shows up in the details: a lined chamber that resists wear, a media reclaim system that separates fines instead of recirculating dust, and a door seal that doesn't leak abrasive after a thousand cycles. If you're running delicate aluminum castings next to steel brackets, you also need a drum speed that won't beat parts into scrap. A manufacturer that asks about your part geometry, weight, and finish spec before quoting is already ahead of one pushing a stock model.
Price matters less than what happens after installation. A cheap machine burns through media faster, demands more energy, and hides wear parts behind panels that take an hour to open. Ask about liner replacement intervals, blast wheel amp draw, and whether the manufacturer stocks common parts locally. Maintenance should be boring: a quick daily check of the media level, a weekly glance at wear plates, and an annual belt inspection. If the design forces you to remove the drum to reach the separator, you'll learn to hate it. The best manufacturers treat finishing as a process, not a transaction—they offer test runs on your actual parts, suggest media blends, and stay reachable when something sounds off. That's the difference between a ten-year asset and a garage ornament.
Contact Us
Contact Person: Bruce
Email: [email protected]
Tel/WhatsApp: +86 15166629468
Website: https://www.povalchina.com/