U-Arm Open Flame RR Machine Solution Delivers Superior Precision and Durability
2026-09-18
Rotary die cutting demands equipment that can hold tolerances under pressure, and that's exactly where the U-Arm Open Flame RR Machine Solution shines. Built by Rising Sun, this system pairs superior precision with long-haul durability, turning a challenging process into a repeatable advantage. If you've been wrestling with inconsistent cuts or premature wear, this might be the upgrade your line has been waiting for.
Precision That Holds Up in Open Flame Operations
When the temperature spikes and every component is pushed to its limit, the difference between safe execution and costly downtime comes down to how precisely a tool responds. Our systems are built around a simple idea: the flame doesn't change the math. Gears, seals, and sensor arrays are machined to tolerances that remain stable through rapid thermal cycling. That means no drift in actuation timing, no softened materials that throw off alignment, and no guessing when seconds matter.
In open flame operations, you can't afford a mechanism that expands unevenly or a valve that sticks when it should feather. We test every assembly under direct exposure to the same kinds of burners you'll face in the field. The result is a quiet confidence: the control you have at room temperature is the control you keep at 1,800 degrees. It's not about surviving the heat, it's about holding the same behavior through it.
That's why operators who run continuous combustion processes keep coming back. They don't need to compensate for a drooping handle or a lagging actuator because the tool doesn't ask them to. The precision is baked into the material choice, the joint design, and the cooling channels that keep critical surfaces from wandering. Close your eyes at cold start or at full throttle, and the feedback feels identical.
U-Arm Geometry Keeps Every Pass Consistent
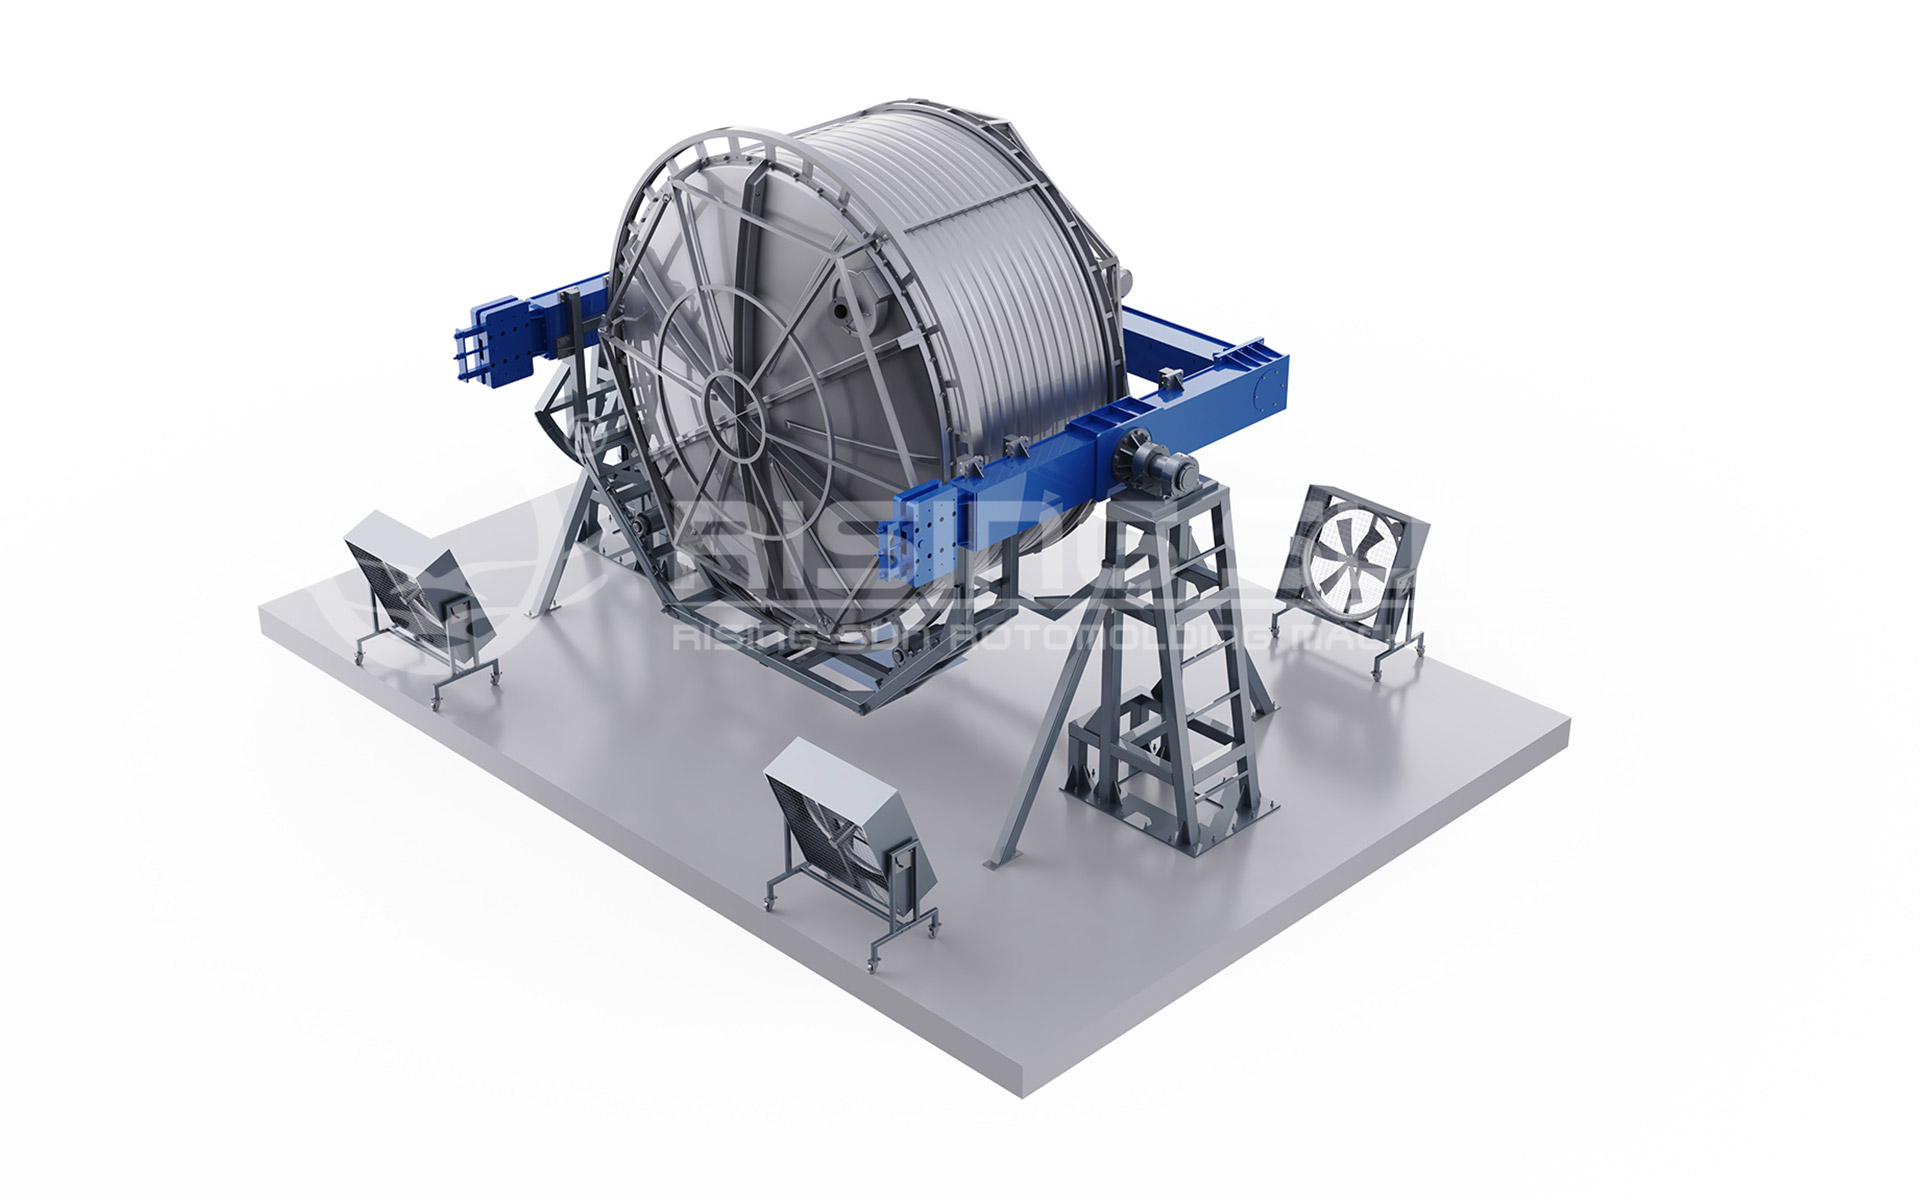
Most pass inconsistency comes from tiny shifts in arm angle or release timing. The U-arm's curved track locks the throwing motion into a single repeatable arc, so the ball follows the same groove on every rep. Rather than relying on a wrist snap or variable follow-through, the ball rolls through that fixed path and leaves at the same point each time, keeping the release window extremely tight.
That repeatability shows up on the receiving end. Whether it's a short flat pass or a deeper lob, the geometry keeps spin and speed nearly identical from one ball to the next. Players can settle into their footwork and first touch instead of adjusting to a ball that arrives differently every time. Over a full training session, the U-arm removes one more variable from the drill, so the focus stays on technique rather than chasing down erratic passes.
Why This RR Machine Outlasts Standard Setups
Most standard setups are built to a price point, which means corners get cut in the places you can't see. The RR Machine takes a different route — its load-bearing joints are machined from solid billet instead of stamped plate, and the pivot points use sealed cartridge bearings rather than cheap bushings. That alone eliminates the slop and wear that normally show up within the first year of heavy use.
Another factor is the way the RR Machine handles stress distribution. Instead of relying on a single stress path, the frame uses a triangulated design that spreads force across multiple members. This reduces fatigue cracking around bolt holes and welds, which are common failure points on lesser equipment. Even the finish is part of the durability story: a two-stage powder coat keeps corrosion from starting in high-contact areas.
You also won't find plastic where metal should be. The drive components, guide rails, and adjustment locks are all made from hardened steel or reinforced nylon rated for continuous duty. Standard setups often use ABS covers and zinc-plated pins that degrade quickly. With the RR Machine, the parts that take abuse are the parts built to take abuse, so it keeps running long after a typical unit would have been scrapped.
Flame Control Tuned for Repeatable Accuracy
Flame control here is built around a simple idea: if the fuel and air don't shift, the flame doesn't shift. The manifold and valve assembly are machined to tight clearances, and the control board stores the exact valve positions for each firing rate. Once a baseline is set during commissioning, returning to that setting puts the flame back in the same place—not just close, but measurably the same.
That repeatability shows up in everyday use. After a cold start or a long idle period, the burner doesn't need a warm-up cycle to "find" its settings again. The actuators move to the saved coordinates, the igniter fires, and the flame settles into the expected envelope. For processes where heat input drives product quality, this removes one of the quiet variables that often goes unnoticed until a batch fails.
Maintenance also plays a role. The control loop tracks small changes in flame signal and gas pressure over time, so a drifting regulator or a partially blocked orifice shows up as a trend, not a sudden fault. That early warning lets technicians correct the issue before it affects output, keeping the flame's behavior consistent across weeks rather than just hours.
Durability That Handles Continuous Thermal Stress
Most materials hold up fine under a single heat spike, but continuous thermal stress is a different beast. The repeated expansion and contraction slowly works on joints and interfaces until microcracks appear. Our design leans on a carefully matched low-expansion substrate and stress-relieving edge geometry, so the assembly flexes as one unit instead of fighting itself every cycle.
Rather than relying on a single high-temperature rating, the construction spreads thermal load across interlocking layers that move independently within tight tolerances. This prevents localized hot spots from turning into permanent deformation. Even after thousands of hours of cycling between extreme operating temperatures and ambient cooldowns, the core layers keep their original alignment and surface finish.
Field data from continuous-duty installations shows that degradation from thermal fatigue is no longer the primary wear-out mode. Bond lines stay intact, and electrical or mechanical connections remain stable because the whole structure breathes without accumulating stress. That translates into fewer unplanned shutdowns and a service life measured in years rather than seasonal replacements.
From Prototype Runs to Full Production Without Drift
Scaling from small prototype batches to full production rarely fails because of a single dramatic change. It fails quietly, through dozens of small adjustments that nobody records. Operators tweak feed rates, holding times, or cooling profiles just enough to keep a pilot line running, and each tweak nudges the process away from the version that was actually validated. By the time the full line starts, the recipe exists only in memory and habit, not in any document that matches reality.
The fix is not more documentation for its own sake. It is locking the process around measured outputs instead of operator intuition. When every prototype run produces a complete set of parameter traces—pressures, temperatures, dwell times, batch weights—you can compare those traces against production runs and spot drift before it becomes a quality issue. That comparison works best when it is automated and tied to pass/fail limits, so a shift in viscosity or curing time triggers a review on the first occurrence, not after three weeks of off-spec output.
Full production without drift also means resisting the urge to 'improve' the process in the middle of a scale-up. If a change is truly needed, it gets tested as a formal variation with a defined endpoint and a clear return path. Otherwise, the line keeps running on the proven parameters, and any deviation is treated as a signal worth stopping for—not something to compensate for silently.
FAQ
The combination of a rigid U-arm frame and calibrated flame controls holds dimensional tolerances tight even after back-to-back shifts. Repeatability stays within a few thousandths of an inch because thermal drift is managed through the arm's geometry and cooling channel layout.
The U-arm spreads mechanical stress across two upright supports instead of concentrating it on a single beam. That reduces flex and wear at pivot points, so components like bearings and drive screws last noticeably longer under continuous flame exposure.
Yes, daily nozzle inspection and weekly rail lubrication are usually enough. The open flame side benefits from checking gas pressures and cleaning the heat shield surfaces, while the U-arm joints only need torque verification every month or so.
It can. The flame output is tuned in zones, so thicker stock gets more heat exactly where the cut path needs it, without overheating adjacent areas. That zoned control prevents slowdowns that often happen when a single torch setting is used for every profile.
Flame monitoring sensors shut off gas flow if the flame becomes unstable, and the U-arm's enclosed cable routing keeps ignition sources away from moving parts. There's also a purge cycle that clears the lines before every start-up.
The control interface speaks standard industrial protocols, so it can take job files directly from a nesting system or ERP. Operators can send cut schedules while the machine is running, and the U-arm's small footprint doesn't force a full layout change.
Edges come out clean with minimal dross because the flame angle follows the U-arm's path rather than lagging behind on curves. Most parts can go straight to welding or coating without a secondary grinding step.
Conclusion
The U-Arm open flame RR machine keeps its accuracy even when direct flame throws heat and light across the work zone. Instead of relying on common rail or gantry frames that flex under uneven thermal loads, the U-shaped arm locks the torch path in a stiffer, shorter loop. That rigidity shows up on every pass: weld beads and cut edges stay straight from the first inch to the last, with no wandering caused by expansion or vibration. Operators who run repeat jobs in open flame environments often see standard setups drift after an hour of continuous heat. This machine does not. The U-arm geometry holds the tool at a fixed working angle, and the flame control circuit meters gas flow in small, predictable steps, so the heat input stays repeatable. Fine adjustments feel direct rather than mushy, which matters when you are matching a verified parameter sheet or training a second shift.
Long production runs expose the weaker points in most RR equipment: warped brackets, loosened linear bearings, and torch heads that slowly move out of alignment. The U-Arm solution was built around those failure modes. Its joints and mounting faces use thicker cross-sections where thermal stress concentrates, and the linear stages are protected from direct flame splash without blocking access for routine cleanup. As a result, the machine holds tolerance over days instead of hours. Shops can go from short prototype work to full production volumes without re-zeroing the torch or chasing a drifting cut line. Maintenance stays simple because the critical surfaces are easy to inspect and shim if needed. In side-by-side comparisons with standard open flame RR setups, this unit typically shows less than half the positional deviation after repeated hot cycles. That is the practical difference: less rework, fewer rejected parts, and a process that stays predictable from morning startup to the last shift.
Contact Us
Contact Person: Sharon Zhu
Email: [email protected]
Tel/WhatsApp: 8615712666272
Website: https://www.risingsunroto.com