U-arm Open Flame RR Machine Supplier for Superior Performance
2026-09-21
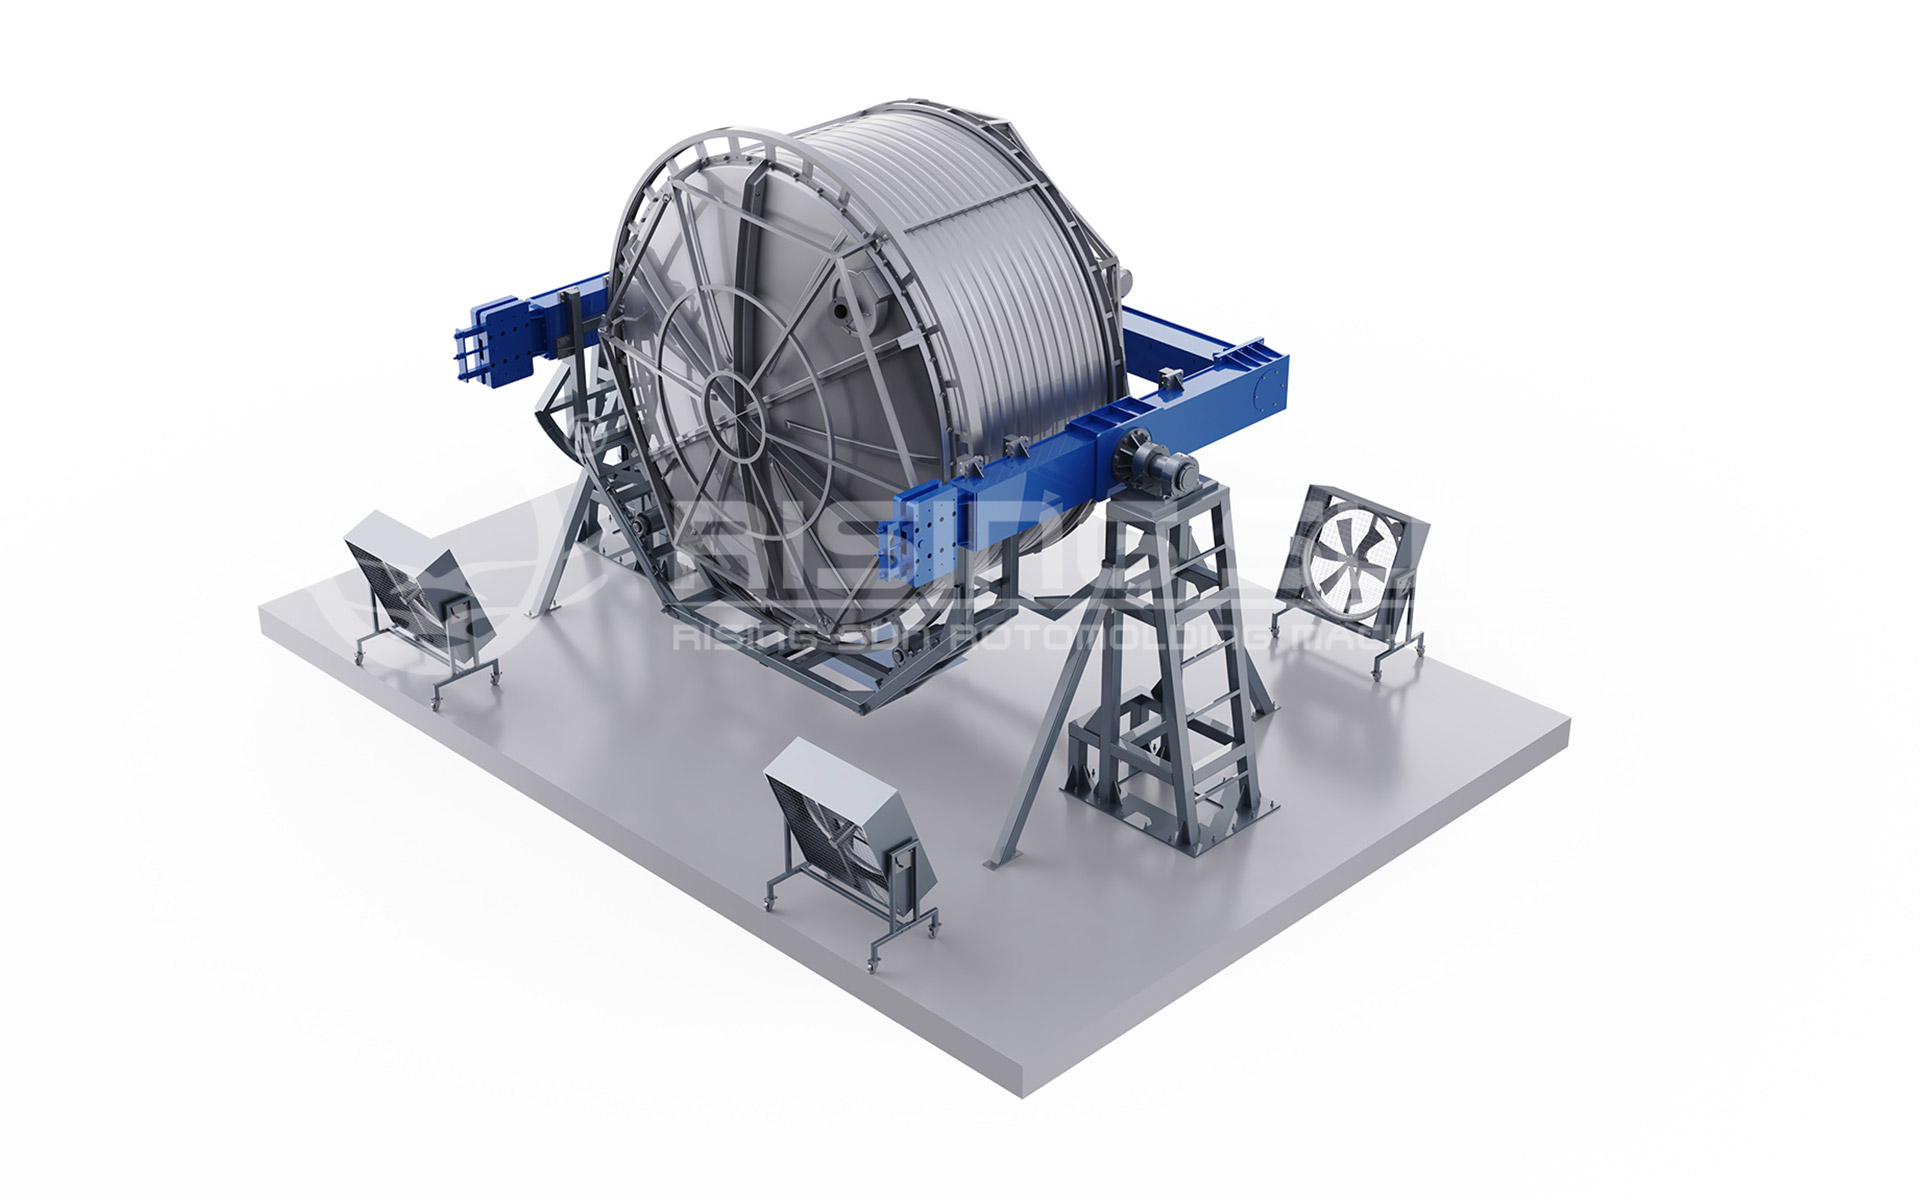
Everyone promises superior performance until the first production run exposes uneven flame contact. The U-arm open flame RR machine is a different story—especially when it comes from a supplier that actually builds for repeatability. That’s where Rising Sun enters the picture. Before you commit to a machine, here’s what to check in flame geometry, temperature control, and long-run stability.
When the U-Arm Frame Stops Being a Minor Detail
Most buyers glance at the U-arm frame and move on to flashier specs like weight capacity or tilt range. Yet the moment a monitor starts to sag after a week of use, that overlooked piece of metal becomes the only thing you think about. The frame's wall thickness, the fit of its pivot joints, even the way the coating resists micro-scratches—all of it quietly decides whether the setup feels solid or vaguely disappointing.
It is only after living with a poorly designed U-arm that the difference becomes obvious. A good one holds position without creaking, lets you adjust the screen with one hand, and does not gradually drift toward the desk overnight. In that sense, the U-arm frame never was a minor detail; it was the quiet backbone of the entire experience.
Burner Adjustments That Don't Need Constant Watching
There's a quiet satisfaction in setting a burner just right and then walking away, not out of neglect, but because you've learned its rhythm. With a little foresight, you can dial in a low, steady flame that holds a simmer without boiling over or scorching the bottom of the pan. The trick is to make small adjustments early, then let the heat do its work while you turn to chopping, washing, or simply leaning against the counter with a cup of tea.
Cast iron and heavy-bottomed pots are your allies here. They take longer to heat up, but once they're warm, they distribute that warmth so evenly that a medium-low setting behaves like a patient friend. You can set a rice pot on the smallest burner, nudge the knob until the flame is a whisper, and trust that the grains will steam to tenderness without a single stir. The same goes for slow-cooked sauces—give them a gentle bubble and a tilted lid, and they'll reduce in their own time.
The real secret isn't in the burner itself; it's in reading the signs before you step away. A shimmer on the oil, a soft hiss from the pan, the way steam curls around the lid—those tell you more than any timer. Once you recognize when a dish has settled into its cooking groove, you can leave it alone. No hovering, no lifting the lid every two minutes. Just a kitchen that takes care of itself while you take care of something else.
Duty Cycles from a Supplier's Point of View
When a supplier evaluates duty cycle, the conversation rarely stays at the stated percentage. What matters is the thermal pattern behind it. A motor rated for S3 40% does not simply get more leeway because the ambient temperature happened to drop a few degrees. Each start and stop cycle introduces mechanical stress on bearings, windings, and connections. So we ask questions that customers often have not mapped out: How many starts per hour? How long does the load actually run before shutting off? Is there a cooling period between cycles, or does the operator restart it nearly immediately?
One of the most common failure points we see is an optimistic duty cycle estimate during the quoting phase. A buyer wants the smaller frame and the lower price, so the intermittent rating gets stretched. The equipment ships, and a few months later the insulation starts showing heat damage. From our side, we would rather receive a recorded load profile from a data logger than a nameplate guess. Intermittent duty can absolutely allow a compact, cost-effective unit, but only if the on-time and rest-time match reality. We also look closely at jogging, plugging, and locked-rotor events, because those add heat that a simple percentage never captures.
Being honest about duty cycle protects both the supplier and the customer. If an application calls for continuous operation but the order specifies S2 30 minutes, we flag it before production. Sometimes a slightly larger frame with a lower temperature rise ends up costing less over five years than adding external cooling to an undersized machine. The point is not to upsell; it is to match the thermal envelope to the way the equipment will actually live on the floor, including weekend shifts, seasonal heat, and operators who push the start button more often than anyone planned.
What Long Runs Do to the Open Flame Array
Long runs push the open flame array into a steady state where heat stops dissipating the way it does during short bursts. The burner heads and flame spreaders stay hot enough that the metal expands slightly, and the flame ports can shift by a fraction of a millimetre. That tiny change is enough to make the flames lean unevenly, with some ports burning a hard blue while others show a lazy yellow tip. Over several hours, the array begins to sound different too—a softer, flatter roar instead of the crisp hiss you get at startup.
Carbon buildup becomes the bigger issue the longer the array runs without a cool-down cycle. Fine particles from the gas stream, along with dust drawn in from the surrounding air, bake onto the edges of the flame ports. This narrows the openings and forces the gas out at a higher velocity in some spots and a weaker stream in others. You start to see gaps in what should be a continuous ribbon of flame, and those gaps tend to grow as the deposits harden. A quick wipe when the array is cold won't remove it—the carbon has to be scraped or burned off with a brush made for the purpose.
There is also a thermal fatigue factor that only shows up after many long runs. The metal expands when hot and contracts when cold, and if the array never gets a proper rest, the repeated stress settles into the castings or welds. Hairline cracks can appear around the base of the flame spreader, and once that happens the flame pattern becomes unpredictable. One port may throw a longer flame than its neighbours, and occasionally the array will produce a soft pop when the gas reignites inside a hot crack. For anyone running the array for extended periods, keeping an eye on those small cracks is more important than the usual cleaning routine.
Why Dense Schedules Favor a Different RR Setup
When training volume climbs and rest days shrink, the classic heavy-light-medium rotation starts to crack. Dense schedules leave less room for full recovery, so a setup built around frequent, moderate stimulation often outperforms one that chases peak intensity. Shifting to shorter rest intervals, altering exercise order, or swapping in variations that reduce joint stress can keep progress moving without forcing extra days off.
A different RR setup for packed calendars typically leans on autoregulation. Instead of prescribing fixed loads for every session, you adjust based on how the body feels that day. This matters more when sessions are back-to-back, because a bad night's sleep or a missed meal has a bigger ripple effect. Using rate of perceived exertion or bar speed as a guide lets you train hard on good days and back off on rough ones, avoiding the slow burnout that rigid programming invites.
Exercise selection also shifts under dense scheduling. Compound lifts that hammer the same muscle groups with heavy eccentrics become harder to recover from, so swapping in more unilateral or machine-based work can preserve training frequency. The goal isn't less effort, but smarter distribution of stress across the week. A well-tuned RR setup for this context keeps every session productive without turning any single day into a recovery debt that compounds.
Notes from Facilities That Push These Machines Hard
The maintenance logs from heavy-duty workshops tell a story that spec sheets never will. Machines running double shifts in dusty yards develop quirks—a slight hesitation in the hydraulic arm, a rattle that only appears under full load, a control panel that overheats after six straight hours. These are not defects but fingerprints of round-the-clock use, and the crews who keep them running learn to read those fingerprints like weather maps. They replace seals before they crack, swap filters on a schedule that ignores the manual, and keep spare solenoids in a coffee can by the bench.
Facilities that truly push equipment past its comfort zone rarely rely on factory intervals. Instead, they build their own repair cadence from broken bolts and blown hoses, marking each failure on a wall chart until patterns emerge. One operator might note that a particular pump fails every eighteen hundred hours, while another tracks how often the drive belts stretch in high-humidity months. That tribal knowledge gets passed down in grease-stained notebooks and shouted over the din, and it keeps a machine alive long after the warranty expires.
There is also a quiet respect for the machines themselves in these places. A loader that has moved ten thousand tons of gravel gets a pat on the hood at shift change, and a compressor that never quit during a heat wave earns a name painted on its frame. The notes taped inside the cab—"let her warm up five minutes," "don't trust the fuel gauge below a quarter"—read like letters to a trusted mule. That bond is not sentimental; it is practical. A machine pushed hard but understood well will outlast a babied one that no one bothered to learn.
FAQ
The open flame design paired with the rigid U-arm construction ensures even heat distribution, which translates into consistent material treatment and fewer rejects on the line.
It's particularly effective in textile finishing, nonwoven processing, and technical fabric production where controlled flame treatment is essential for surface modification.
The U-arm frame reduces vibration and maintains precise alignment during high-speed runs, so operators see less drift in flame intensity and more uniform output.
Yes, the supplier offers modular adjustments for width, burner arrangement, and speed controls so the system fits your existing line rather than forcing a one-size-fits-all setup.
Routine checks of the burner tips, flame sensors, and U-arm bearings every 200 operating hours are usually enough, with a full inspection recommended quarterly.
Absolutely, built-in flame monitoring, automatic shutoff, and heat shielding around the U-arm make it suitable for round-the-clock operation without compromising worker safety.
The supplier provides on-site commissioning, hands-on operator training, and remote troubleshooting for the first month to ensure your team gets the most from the machine's capabilities.
Most facilities report a 15–20% increase in line speed and a noticeable drop in energy waste because the flame is focused exactly where it's needed.
Conclusion
The U-arm frame is often dismissed as a supporting component, but on an open flame RR machine it directly controls how evenly the burner array tracks across the fabric. When the frame flexes even slightly during long production windows, the flame pattern shifts and edge temperatures drift. A supplier focused on superior performance will reinforce the U-arm geometry and pivot points so that the assembly holds its position without daily rechecking. Burner adjustments, once set for a particular fabric weight, should remain stable through shift changes. The best setups use indexed gas controls and shielded pilot assemblies that resist vibration and thermal expansion, reducing the need for operators to watch gauges throughout the run.
Duty cycle ratings from a supplier's perspective matter more than peak output numbers. Machines built for continuous RR work need larger bearing surfaces, cooler-running drive components, and flame arrays that can withstand repeated heating without warping. Facilities that push these machines hard report that dense schedules quickly expose weak points in lighter frames and short-lived burners. In those environments, a different RR setup, often a heavier reciprocating mechanism with staged burners, holds up better than a compact unit designed for intermittent use. Long runs also produce soot buildup and gradual nozzle wear, so access panels and quick-change burner rails become practical advantages rather than conveniences. A supplier who understands these operating realities builds the U-arm open flame machine around sustained output, not just demonstration performance.
Contact Us
Contact Person: Sharon Zhu
Email: [email protected]
Tel/WhatsApp: 8615712666272
Website: https://www.risingsunroto.com